Why Does Strip Bow After the Straightener?
Strip that bows after the straightener is telling you which roll pair is doing the work, and the answer is rarely the last one. Bow is a geometry problem before it is a pressure problem.
On a 1.2 mm SPCC job running 8 mm of bow per metre, the fault usually sits in the entry pair, not in the finishing pair where everyone adjusts first.
An NC straightener feeder can only remove the curvature its roll geometry is set up to remove. Everything outside that is a limit, not a tuning issue.
Here is how to read the strip, separate the four causes, and set the rolls against the bow you actually measured.
Read the Strip Before You Touch a Roll
Three faults get called bow on the shop floor, and they have different causes. Cutting a sample and looking at it costs two minutes.
Bow. The strip curves along its length, like a banana when viewed from the side. Set a 300 mm sample on a surface plate and measure the gap at the centre.
Crossbow. The strip curves across its width, so the edges lift off the plate. That is a roll crown or a gap that is uneven across the face, not a penetration problem.
Twist or camber. The strip curves sideways in plan view. It comes from unequal edge strain, usually a guide that is pinching one edge or a coil with edge damage.
Write the number down before adjusting anything. Bow of 8 mm over a 300 mm sample is a curvature of about 0.35 per metre, which is roughly 12 I-units. That is a real fault, not measurement noise.
The direction of the bow matters as much as its size. A bow that curves up means the top surface was stretched last. A bow that curves down means the bottom surface was.
That single observation tells you which roll pair to look at, and it eliminates half the adjustments people make by habit.
The Four Causes and How to Separate Them
Four faults produce the same visible symptom. The way to separate them is to change one variable and watch whether the bow responds.
| Cause | What the strip shows | What it costs you if you ignore it |
|---|---|---|
| Penetration too shallow | Even bow along the whole sample, direction matches the last roll contact | Feed length error at the die and a part that springs back after forming |
| Uneven gap across the width | Crossbow, one edge lifting 0.3 mm or more | Edge wave on one side and a cambered part that will not sit in the fixture |
| Worn or crowned rolls | Bow that changes along the coil length, worse at the coil ends | Scrap that appears in batches and is blamed on the coil supplier |
| Back tension pulling the strip | Bow that disappears when the line stops | A straightener set too shallow to compensate, hiding the real fault |
The fourth row is the one that gets missed. A line with high back tension pulls the strip flat through the rolls, and the bow only appears when the line stops and the tension releases.
Test it by threading a metre of strip with the brake released and measuring that sample. If the bow appears only with tension on, the straightener is not the problem.
The second row separates itself: crossbow does not respond to penetration at all. Add penetration and the crossbow stays. That is the test, and it takes one coil.
Roll wear is the slow one. It shows up as a bow that varies with coil length because the worn zone sits at one position across the face, and a wide coil uses more of it than a narrow one.
Setting Gap and Penetration Against the Bow You Measured
Once the cause is known, the settings follow. These are the numbers that matter, in the order they should be changed.
Roll gap on the finishing pair. Set it to strip thickness minus 0.02 mm for CR material. A 1.2 mm strip gets 1.18 mm. Wider than thickness means the strip passes without being worked.
Penetration on the working rolls. Bring the upper roll down until it is 0.6 to 0.9 mm below the pass line for 1.2 mm CR, depending on roll count. More rolls need less penetration per roll.
Entry pair. Open it slightly when the coil arrives with strong set. A tight entry pair fights the coil and transfers the curvature downstream instead of removing it.
Roll count. Five rolls remove bow on mild CR up to about 2 mm. HSLA 340 and above usually needs seven, and 420-grade work hardens enough that nine is not unusual.
- Change penetration first and measure the same 300 mm sample after 5 m of running, not after the first metre.
- Check the gap at both ends of the roll face with a feeler gauge. A 0.05 mm difference across 1,300 mm is enough to produce crossbow.
- Log the setting that produced a flat sample against the coil number, so the next coil from the same mill starts from a known point.
- Re-check after a coil change. A different mill batch often needs a different entry gap for the same nominal grade.
Do not chase bow with back tension. Tension straightens strip on the line and releases it at the die, which moves the problem into the press where it is harder to see.
What a Straightener Cannot Fix
A roll straightener removes curvature by bending the strip past yield in alternating directions. Anything that does not yield stays as it was.
Coil set stronger than the roll count can reach. A coil that has sat for a year in a humid warehouse develops a set that a 5-roll head cannot remove at any penetration. Seven rolls are the answer, not more pressure.
High-strength grades near their limit. HSLA 420 and above work-harden with each pass. Past a point the strip cracks at the edge before it flattens, and the straightener becomes a scrap generator.
Thickness above about 4 mm. The force needed to yield 4 mm strip exceeds what a standard head can apply, and the frame deflects instead of the strip.
Narrow strip with edge damage. A 60 mm strip with a burred edge cannot be flattened by rolls that contact the burr first. The bow is a symptom of the edge.
There is a fifth case that is not about the machine at all: a die that needs flat strip in one direction and a part that springs back in another.
Sometimes the bow is the die's problem, and no straightener setting will satisfy both.
Honest limit, stated plainly: a straightener improves flatness, it does not create it. If the incoming coil is 25 I-units out, no head will deliver 5.
The Ten-Minute Test That Settles It
Before calling a service engineer, run this sequence. It separates a setup fault from a machine fault with equipment already on the floor.
| Check | Pass looks like | If it fails, where to look |
|---|---|---|
| Sample bow on a plate | Under 2 mm over 300 mm | Penetration or roll count for the grade |
| Gap across the roll face | Within 0.02 mm end to end | Roll crown, bearing shim, or a bent frame |
| Bow with tension released | Same as with tension on | Brake or drag setting masking the fault |
| Roll surface and diameter | No step over 0.01 mm, no polish ring | Worn rolls, or a slip point on one roll |
| Same coil at two widths | Same bow at both | Guide pinch or edge damage if it changes |
Run the five checks in that order and write the results down. The pattern points at one cause, and the pattern is repeatable across shifts.
If the gap is even, the rolls are clean, the tension is released and the bow persists at 8 mm per metre on a 1.2 mm mild coil, the head does not have the roll count for the job.
That is a specification answer, not a maintenance one.
Most of what we see on site is the opposite: a correctly specified head set up by trial and error, with the penetration left where the last operator put it.
A 300 mm sample and a feeler gauge resolve that in ten minutes.
The flatness specification itself is worth reading before a roll count is chosen.
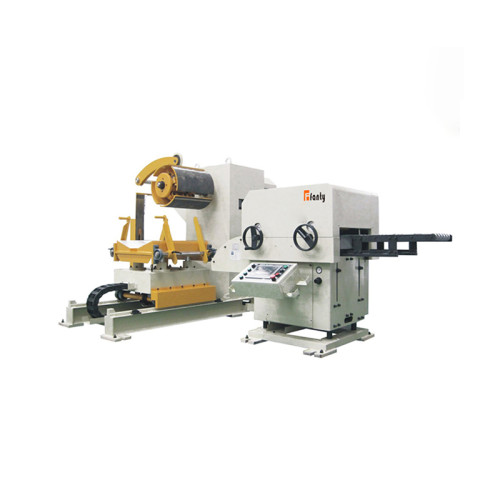
Roll count, pitch and penetration interact, and the 3-in-1 decoiler straightener feeder guidance sets out how those three numbers are chosen together.
How much bow is acceptable after straightening?
Under 2 mm over a 300 mm sample for most stamping, which is about 3 I-units. Drawing work that needs a flat blank usually wants under 1 mm.
How much penetration does 1.2 mm CR strip need?
0.6 to 0.9 mm below the pass line on a 5-roll head, and less per roll as the count rises. Start at 0.7 mm and measure before going further.
Does a 5-roll head handle HSLA 340 at 2 mm?
Usually not. Seven rolls is the practical minimum at that yield strength and thickness, and the penetration needed on five rolls starts to mark the surface.
At what thickness does a standard head stop removing bow?
Around 4 mm for mild steel. Above that the frame deflects more than the strip yields, and a different head design is needed rather than more pressure.
Where to go next
Bow is one output of a roll set, and the same geometry that removes it also decides whether the strip tracks straight into the die.
Flatness is covered in full inside the coil line guide library, from roll count and pitch through to the gap and penetration numbers used above.