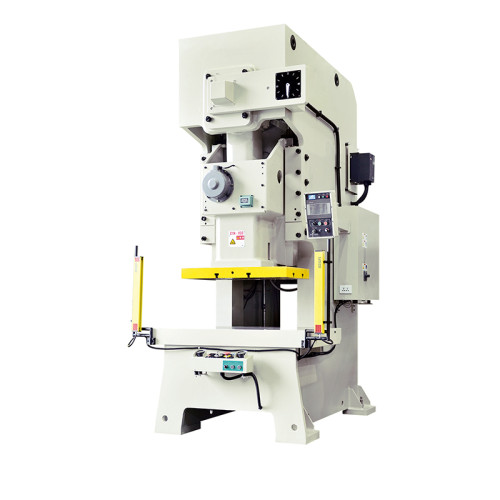
Why Do NC Straightener Feeder Specs and Output Differ?
“The quotation said ±0.05 mm at 200 SPM. On our floor the best we ever measured was ±0.15 mm, and the press never ran past 90 strokes a minute.” That came from a purchasing manager at a Turkish job shop six weeks after his NC Straightener Feeder was commissioned. He was not describing a broken machine. He was describing a specification written for one set of conditions and then read as though it applied to another.
This is the story of that order — the four quotations he compared, the first production week, the measurements that started the argument, and the machine he bought the following year. It ends with four lines of wording that would have avoided the whole thing, and which belong in any NC Straightener Feeder purchase order.
The Order, and the Four Quotations Behind It
The shop runs progressive dies for agricultural brackets. Material is SPHC pickled and oiled, mostly 2.5 mm, sometimes 3.2 mm, in coils up to 1,250 mm wide and 4.5 t. Two presses, 110 t and 160 t, both older mechanical machines with a nominal top speed of 180 SPM. The job that triggered the purchase was a bracket family with a 14-station die that had been running from cut blanks.
Four suppliers quoted. All four were asked for a 3-in-1 machine with a 1,300 mm width capacity and a 6 mm thickness rating. The comparison sheet the buyer built had one technical column — feed accuracy — and four commercial ones. Three suppliers wrote ±0.05 mm. One wrote ±0.1 mm and lost the technical comparison on the spot.
That single column decided the order. It should not have, and the buyer now says so openly. A feed accuracy figure without a thickness, a width, a speed and a material attached is not a specification, it is a capability ceiling measured under conditions nobody wrote down.
Week One on the Floor
Installation took four days and the commissioning engineer set recipes for three jobs before he left. The first production week produced a pattern the shop had not planned for.
- Feed length held well below 100 SPM. Dial indicator checks on the first station showed 0.04 to 0.07 mm of variation at 60 to 80 SPM. Nothing to complain about.
- Above 100 SPM it opened up. By 130 SPM the same check read 0.12 to 0.18 mm, and the die started shaving the pilot holes.
- Flatness drifted on the 3.2 mm coil. The thicker material came off the straightener with a visible bow that the 2.5 mm coil never showed.
- Scrap rose in a step, not a slope. The die ran clean for a shift, then produced a run of short feeds that broke two punches.
By the end of the week the shop had dropped to 85 SPM to protect the die, which is roughly where the old hand-fed process had been. The machine was working. The throughput the quotation implied was not there.
Where the Two Numbers Separated
The commissioning engineer returned with a data logger and ran the line through a stepped speed test. The measurements explained the week in one table.
| Test condition | Feed length variation | What was happening |
|---|---|---|
| 2.5 mm × 1,000 mm, 60 SPM | 0.04 – 0.07 mm | Nominal condition, coil at mid weight |
| 2.5 mm × 1,000 mm, 130 SPM | 0.12 – 0.18 mm | Roll slip on acceleration, loop unstable |
| 3.2 mm × 1,250 mm, 60 SPM | 0.09 – 0.14 mm | Straightener deflection across full width |
| 3.2 mm × 1,250 mm, 130 SPM | 0.19 – 0.26 mm | Both effects combined |
| 2.5 mm, full 4.5 t coil, 130 SPM | 0.15 – 0.22 mm | Coil mass and brake torque fighting the loop |
Read down the second column and the pattern is obvious. Every increase in thickness, width or speed moved the variation. The machine was not drifting; it was being pushed outside the window its accuracy figure was measured in.
Is a quoted feed accuracy figure meaningless, then?
No, but it needs conditions attached. A number measured on 1.0 mm × 400 mm strip at 100 SPM tells you nothing about 3.2 mm × 1,250 mm at 130 SPM. Ask what material, thickness, width and speed the figure was taken at, and ask for the test record.
Should a wider machine be quoted for the same job?
Only if the width is actually needed. Width capacity is a structural question, not a cosmetic one: a 1,300 mm straightener with the same roll diameter deflects roughly twice as much as a 700 mm one under identical strip tension. If every job runs at 900 mm or less, buying 1,300 mm capacity costs accuracy you will never use.
Does the press speed limit come from the feeder or the die?
Usually from whichever runs out first, and the order is not fixed. In this shop the die piloting set the practical ceiling, and the feeder simply exposed it. A line that ran 130 SPM from cut blanks may need pilot release timing reworked before it can run 130 SPM from coil.
What does a stepped speed test cost to run?
Half a day and one coil. It is the cheapest piece of due diligence available on a coil line, and it is the only way to find the speed at which variation starts to climb on your material rather than on the supplier's demo strip.
Why the Quotation Was Technically Correct
Nobody lied. The supplier's figure came from a factory test on 1.2 mm SPCC, 400 mm wide, at 90 SPM, with a full roll set and a properly tuned loop. Under those conditions the machine genuinely holds better than 0.05 mm, and the test record showed exactly that.
The gap opened in four places, and all four were foreseeable.
Strip width changes the straightener, not the feeder. Rolls on a 1,300 mm machine are supported at the ends and deflect in the middle. On 400 mm strip the load sits close to the bearings and deflection is negligible. On 1,250 mm strip the same rolls bend, and the middle of the strip comes out of the straightener with residual bow. The feeder then feeds bowed strip into the die, and the die turns bow into a length error.
Thickness raises the torque demand on every roll. Going from 1.2 mm to 3.2 mm multiplies the cross-section by roughly 2.7 and the force needed to bend the strip by more than that. A machine sized around thin strip will still turn, but it will do so with less margin, and margin is what keeps the rolls gripping during acceleration.
Coil mass loads the brake. A 4.5 t coil carries far more inertia than the 800 kg coil used in a demo. When the press accelerates, the loop has to absorb the difference. If the brake releases too slowly the loop goes slack and the strip loses back tension; if it releases too fast the loop tightens and pulls against the feed rolls.
Speed compresses the correction window. A servo-driven NC straightener feeder has a fixed number of milliseconds to accelerate, feed and settle. At 90 SPM there is time to correct a small slip. At 130 SPM there is not, so the same slip that was invisible becomes a visible length error.
The supplier quoted a capability, the buyer read a promise, and neither side wrote down the conditions that connected them. Twelve years of building coil lines does not remove that risk from a project; only a documented test condition does.
What Changed on the Second Machine
The shop did not scrap the machine. They kept it on the 2.5 mm work, where it holds 0.06 mm all day, and bought a second unit sized for the thicker material. Three things were different on the second order.
Roll diameter went up rather than roll count. Larger rolls on a shorter face resist deflection better than extra passes on a long face, and the shop accepted a 1,000 mm width limit because no current job exceeds 950 mm.
The straightener was specified with a deflection figure, not just a thickness rating. The supplier was asked what the roll deflection is at maximum width and maximum thickness, and to state it in the offer.
The brake was specified by coil inertia rather than coil weight. The buyer sent the coil weight, inside diameter and outer diameter for the three largest coils he buys, and asked for a brake sized on the worst case. That one change removed the loop instability that had caused the 130 SPM problem.
The result was a line that runs 3.2 mm material at 115 SPM with 0.07 mm variation — slower than the original quotation implied, but stable, and the shop now knows why the ceiling sits where it does.
Four Lines to Put in the Purchase Order
None of this is exotic. It is simply a matter of making the offer say what it means.
Accuracy with conditions. Write the requirement as “feed length variation within X mm when running [material] at [thickness] × [width], at [speed] SPM, measured at the first die station over 200 consecutive strokes.” Any supplier who cannot commit to that sentence is quoting a demo, not a machine.
Deflection at maximum width. Ask for straightener roll deflection at full width and full thickness. It is a single number, it is calculable at the design stage, and it tells you whether the width rating on the front page is usable across the full face.
Brake sized on your heaviest coil. Supply the coil data with the enquiry — weight, ID and OD for the worst case. A brake matched to a demo coil will work until the first heavy coil arrives.
A stepped speed test at commissioning. Require the commissioning report to include feed variation at three speeds and two thicknesses, signed by the engineer. The test costs half a day and turns a dispute into a data table.
Shops that write those four lines into the order tend to get fewer unpleasant surprises, and they get the second machine approved faster, because the first one delivered what the paperwork said it would. With more than 60 countries of installations behind it, a supplier should have no difficulty producing the test record — and if the record cannot be produced, that is the answer to the enquiry.
Comparing quotations for a coil line? Send us your material, thickness, width and target SPM, and we will return a specification written the way it should be — with the test conditions attached.