Do You Need an NC Servo Feeder or a Roll Feeder?
A tool room manager put it to me plainly last spring: roll feeders are cheaper than they have ever been, so why would anyone still pay for an NC servo feeder? It is a fair question, and the honest answer is that the two machines are not competing on price. They are competing on how much control you need over where the strip sits at the moment the press closes.
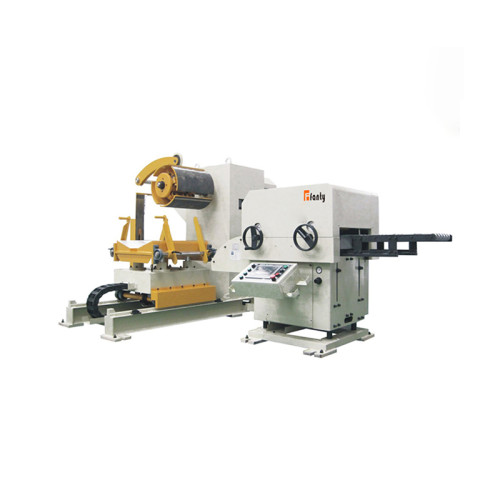
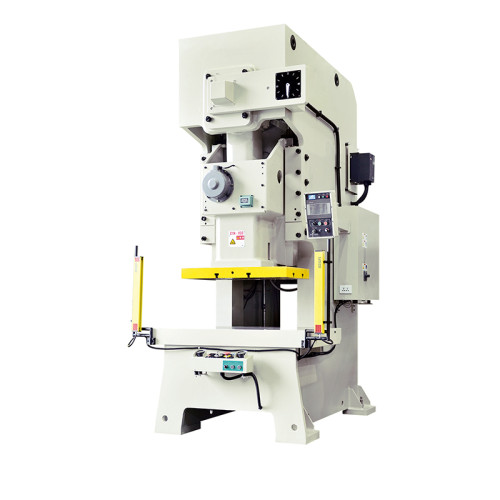
This comparison sets the two feeding principles side by side, shows where each one genuinely wins, and gives you five questions to run in order so the decision follows your work mix rather than the quotation. If you are comparing complete lines rather than the feeder alone, the NC Straightener Feeder range is the right starting point.
Two Feeding Principles, Not Two Price Points
A roll feeder takes its motion from the press itself. The crank drives a mechanism that grips the strip, advances it a fixed distance, releases it, and returns while the press is closed. Feed length is set mechanically, usually by changing a gear ratio or adjusting a stroke, and it is fixed once the press starts running. That mechanical link is also its greatest strength: the feed and the press can never drift out of phase, because they are the same motion.
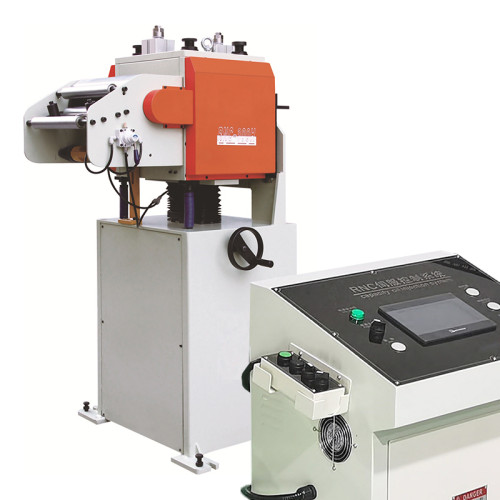
An NC servo feeder breaks that link deliberately. A servo motor drives the feed rolls under program control, so the feed length, the acceleration profile and even the number of separate feed steps are software values. The feeder no longer knows what the press crank is doing; it knows what you told it to do, and it repeats that within a tolerance the mechanism alone cannot reach.
Everything else in the comparison follows from that single difference.
Where Each Type Actually Wins
The table below reflects what shows up in practice, not what appears in a brochure. Ranges are broad on purpose: material, die design and maintenance discipline move the numbers more than the machine type does.
| Requirement | Roll feeder | NC servo feeder |
|---|---|---|
| Feed accuracy | ±0.1 to ±0.3 mm, drifts with wear | ±0.05 mm, held by closed-loop control |
| Feed length change | Mechanical adjustment, 20–60 minutes | Keypad entry, under a minute |
| Multi-step feeding | Not practical | Standard, up to dozens of steps per cycle |
| Speed ceiling | Tied to press stroke and mechanism inertia | Programmable profile, suited to 300–600 SPM presses |
| Thin or soft strip | Prone to marking and slip at high speed | Roll pressure and profile tuned to the material |
| Capital cost | Lower, roughly 40–60% of a servo unit | Higher |
| Maintenance profile | Mechanical wear on cams, gears and grips | Servo, encoder and control electronics |
Read the table as a comparison of ceilings rather than averages. A roll feeder set up carefully, run on one material, at moderate speed, with a die that tolerates its tolerance, is a perfectly good machine. The same feeder asked to hold position on a progressive die with a 0.05 mm window will lose that argument every shift.
The Costs That Do Not Appear on Either Quotation
Purchase price is the easiest number to compare and the least useful one. Four other cost lines decide which machine is cheaper over five years.
- Changeover time. A plant running 40 die changes a month and spending 40 minutes resetting feed length is burning 26 hours a month. At a loaded rate of USD 60 an hour that is USD 1,560 a month, which is the gap between the two machines right there.
- Scrap from position error. On a die with a 0.1 mm clearance, a feed that drifts 0.2 mm on a bad day produces burrs and, eventually, punch damage. The scrap rate difference between the two feed types is small on easy work and large on demanding work.
- Die design freedom. A servo feeder opens the option of a progressive die with tighter pitch and more stations. A roll feeder constrains the die to what the mechanism can hold. Design for the feeder you own, and the die cost changes with it.
- Spare holding. Mechanical feeders wear predictably and can often be repaired on site. Servo feeders rarely fail mechanically but need a stocked encoder, drive or control board, because a three-week wait is not survivable on a running line.
Can a roll feeder hold accuracy on a progressive die?
It can on forgiving work: thicker material, generous clearance, and a die with a pilot that corrects position before the working stations. Where the pilot cannot fully correct, or where the strip is thin and the pilot tears it, the mechanical feed runs out of capability and no amount of adjustment will recover it.
Is a servo feeder always the better machine?
No. On a single-part, single-material line running at moderate speed with a die that tolerates ±0.2 mm, a roll feeder is cheaper to buy and cheaper to keep, and it will run for twenty years. Paying for capability the die cannot use is a real cost.
What about a mechanical feeder with a servo retrofit kit?
Occasionally viable on a machine with sound rolls and a good gearbox. Check what the retrofit controls, and whether the existing roll assembly can hold the tighter tolerance. A servo motor driving worn rolls still feeds like worn rolls, only more expensively.
Does strip material change the answer?
Yes. Soft or surface-critical material such as pre-painted or polished strip generally needs servo control because roll pressure can be tuned and marking controlled. Hard, heavy strip at low speed is often better served by a mechanical feed, which has fewer electronics to protect from the plant environment.
Matching the Choice to Your Work Mix
Three work patterns cover most of the field, and each has a natural answer.
One part, one material, high volume. A dedicated line running the same die for months does not need programmable feed length. Buy the simpler machine, spend the difference on coil handling and die quality, and the line will outperform a servo feeder used at a fraction of its capability.
Mixed short runs, frequent die changes. This is where the servo feeder pays for itself fastest. When a plant changes dies several times a week, the time saved at each setup runs into hundreds of hours a year, and the reduced risk of a wrong mechanical setting protects both the die and the strip.
Thin, soft or surface-critical strip. Servo control stops being a convenience and becomes a requirement. Roll pressure, acceleration and the number of feed steps all have to be tuned per job, and only a programmable feeder lets you do that without rebuilding the machine.
In between those patterns, the deciding factor is usually the die rather than the feeder. Ask your tool designer what position tolerance the die actually needs, then buy the feeder that holds it with margin to spare.
Five Questions, in Order
Run these in sequence and the decision usually makes itself. Answer the first two honestly before you look at a quotation.
One. What position tolerance does the die require? Get the number from the tool drawing or the tool designer. If it is tighter than ±0.1 mm, the mechanical option is already out of the running.
Two. How many different jobs run on this line each month? More than a handful of changeovers a month points to servo, not because of accuracy but because of setup time.
Three. What is the press speed, and how much of it do you actually use? A servo feeder only earns its price at the speeds where a mechanical mechanism starts to compromise; a machine that runs at 60% of press capacity rarely sees that limit.
Four. How much strip support does the material need? Thin and soft material needs the feeder to carry it; heavy material can be pushed and pulled with less care.
Five. What can you maintain? A servo feeder needs people comfortable with encoders, drives and parameters. A mechanical feeder needs people comfortable with cams, grips and clearances. Buy the machine your maintenance team can keep running, or budget for the training either way.
Answer those five and you will have a defensible decision, and a document you can show the next person who asks why the line was specified the way it was.
Not sure which feeding method your die needs?
Send the strip material, thickness, feed length and the position tolerance from the die drawing. The FANTY engineering team — twelve years in coil feeding and 200+ installations across 60+ countries — will tell you which method holds it, and when the cheaper machine is genuinely the right one.